Manufacturing
AI Video Analytics for Manufacturing Plants
Get alerts when PPE is missing at production entries, someone enters a machine or maintenance zone, or material piles up at a transfer point, on compatible cameras you already have. Ask Vision Copilot what happened last shift and who should act.
Built for: Plant heads · EHS managers · Production supervisors · Security and IT
See the exceptions that routine rounds can miss.
A factory can have extensive CCTV coverage and still depend on someone noticing a problem at the right moment. Shift changes, shared vehicle routes and busy production areas make continuous manual observation difficult. Plant leaders need to know where an event happened, whether it needs intervention and which team owns the response. Start video analytics with these decisions, then expand to more complex production analysis.
A reference deployment places cameras at production entries, vehicle-pedestrian crossings and one material-transfer point, on a network segment separated from the plant's operational technology (OT) systems. Retention matches the window a safety or quality review typically needs. Send PPE and flow alerts to the production supervisor and EHS, the people who know the shift. Where a shift-scheduling system is available, align review timestamps with its records as well as camera time.
Manufacturing · Use cases
Use cases for factories
Open the Assembly Zone by name
Shift handovers, PPE observations and material build-up are tied to the plant's building tree, so a supervisor opens Assembly Zone or a workcell by name and sees the cameras that cover it.
Search last shift's footage in plain words
Ask Vision Copilot, “Show observations from Assembly Zone during the last shift,” and get the observations for that zone and period instead of scrolling through every production camera.
Spot build-up that keeps coming back
Ask, “Which covered production zones had recurring material build-up this week?” Ongoing scene analysis groups repeat observations by zone, so a recurring transfer-point problem stands out from a one-off alert.
Plan the next shift from the evidence
Ask, “What should the plant team review before the next shift?” Vision Copilot suggests a next step, such as reviewing staging space and replenishment timing, and the production supervisor decides whether to act.
Compare production zones and shifts
Operational scores out of 100, built from PPE and material-flow observations, show which production zones and shifts to review first.
Manufacturing · Vision Copilot
Ask about your factory in plain language
Type a question in everyday language and Vision Copilot searches the observations from your mapped cameras for that place and time.
Questions to try
- What should the plant team review before the next shift?Example answer shown
- Show observations from Assembly Zone during the last shift.
- Which covered production zones had recurring material build-up this week?
Question
What should the plant team review before the next shift?
Location
Plant → Production Building → Shop Floor → Assembly Zone → Workcell
Answer
Material build-up appears repeatedly around the same transfer point during shift handover. Suggested next step: review staging space and replenishment timing at that transfer point, then check the next comparable shift after the change.
Decision owner
Plant / production supervisor
Manufacturing · Location map
Your factory, mapped
Cameras are mapped to the selected location so questions about Assembly Zone start from recognisable operational context.
Site
Plant
Building
Production Building
Floor
Shop Floor
Zone
Assembly Zone
Room
Workcell
Manufacturing · How it works
How OrionAlerts works for factories
OrionAlerts maps each camera to a place, analyses its scenes over time, and sends alerts to the dashboard, mobile app and email for the team that owns that area.
- 01Map
- 02Observe
- 03Ask
- 04Prioritise
- 05Act
- 06Review
Manufacturing · Deployment
Preparing a factory for a pilot
Begin with stable camera views at production entries, crossings and one material-transfer area. Test each shift, including low light, occlusion and PPE variations. Agree who receives each alert and how camera outages are handled.
- Stable camera views at production entries and crossings
- Mapped hierarchy for the pilot production areas
- Defined alert and Copilot review owners
- Representative shift testing including low light and occlusion
- Network segmentation between the camera system and plant OT systems, confirmed with IT/OT before installation
Manufacturing · Standards
Standards context for factories
Video observations give EHS time-stamped context for internal safety reviews within an occupational health and safety programme. ISO 45001 certification covers the organisation's management system and is assessed separately.
ISO 45001
ISO 45001 is an occupational health and safety management-system standard for organisations.
Official source
Manufacturing · Pilot evaluation
What to measure in a factory pilot
Compare reviewed alerts with what actually happened, including missed events and nuisance alerts, before you set a rollout target.
Reviewed PPE exceptions per 100 observable entries
Confirmed relevant PPE exceptions divided by sampled observable entries using a predefined review rubric.
Source of truth: Sampled entry footage and supervisor review log
Median alert-to-acknowledgement time
Acknowledgement timestamp minus delivered/available alert timestamp for reviewed events.
Source of truth: Alert delivery and acknowledgement records
Unavailable camera/recording minutes per monitored shift
Usable recorded minutes compared with required recording minutes for the agreed cameras.
Source of truth: Device health and recording availability records
Manufacturing · Solutions
OrionAlerts solutions for factories
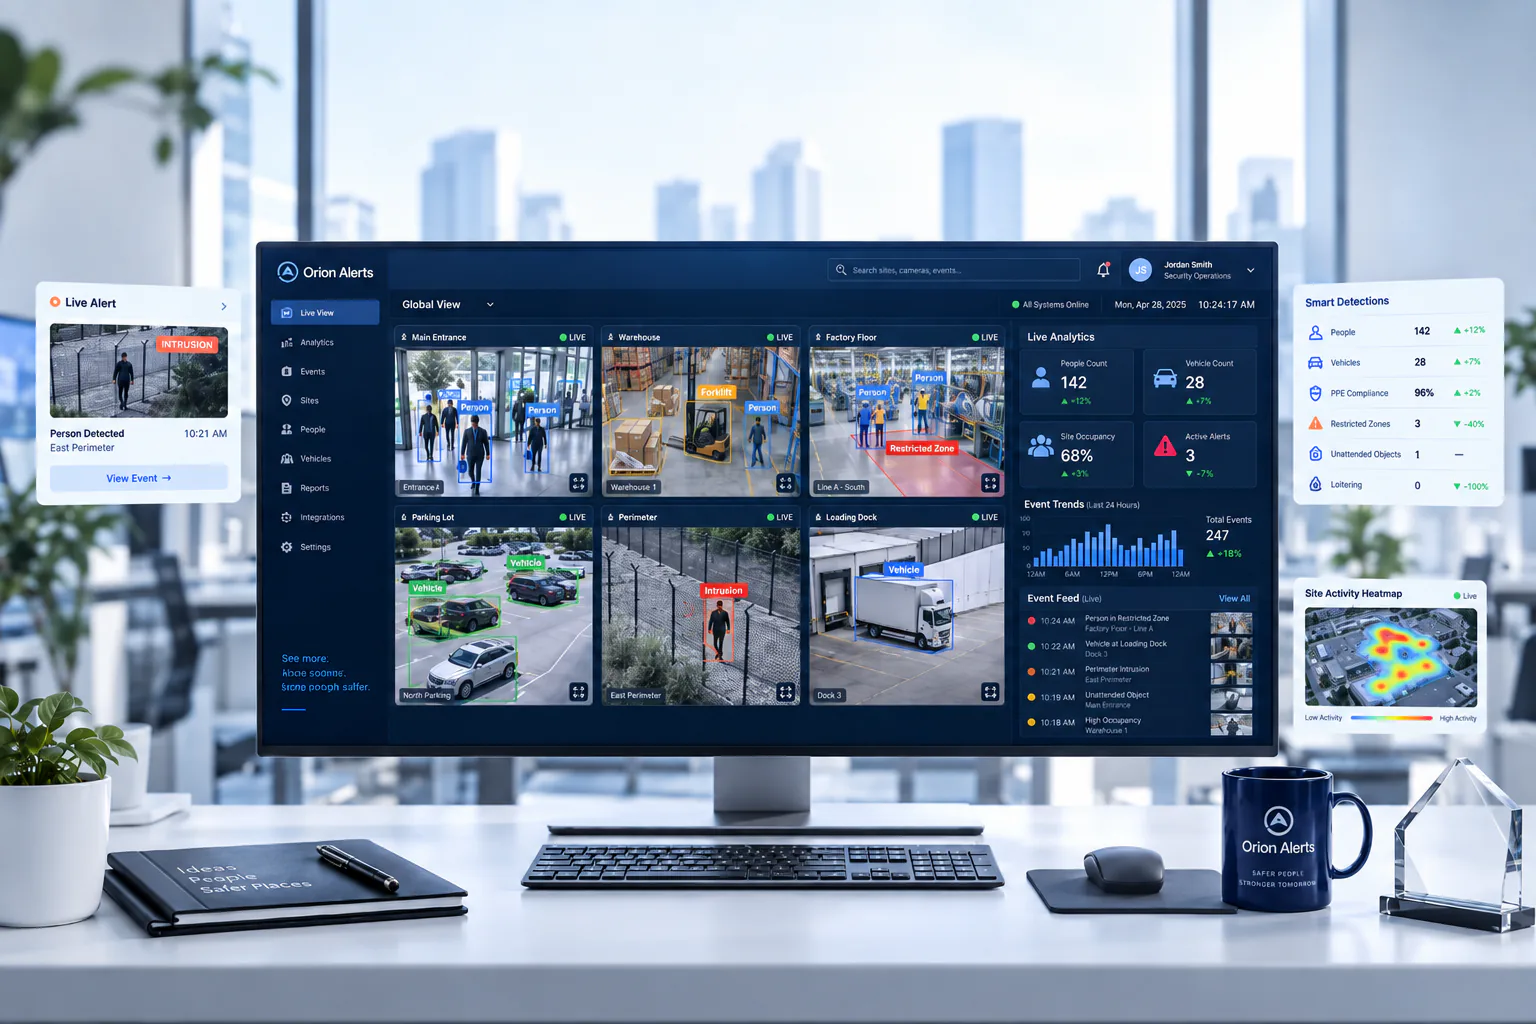
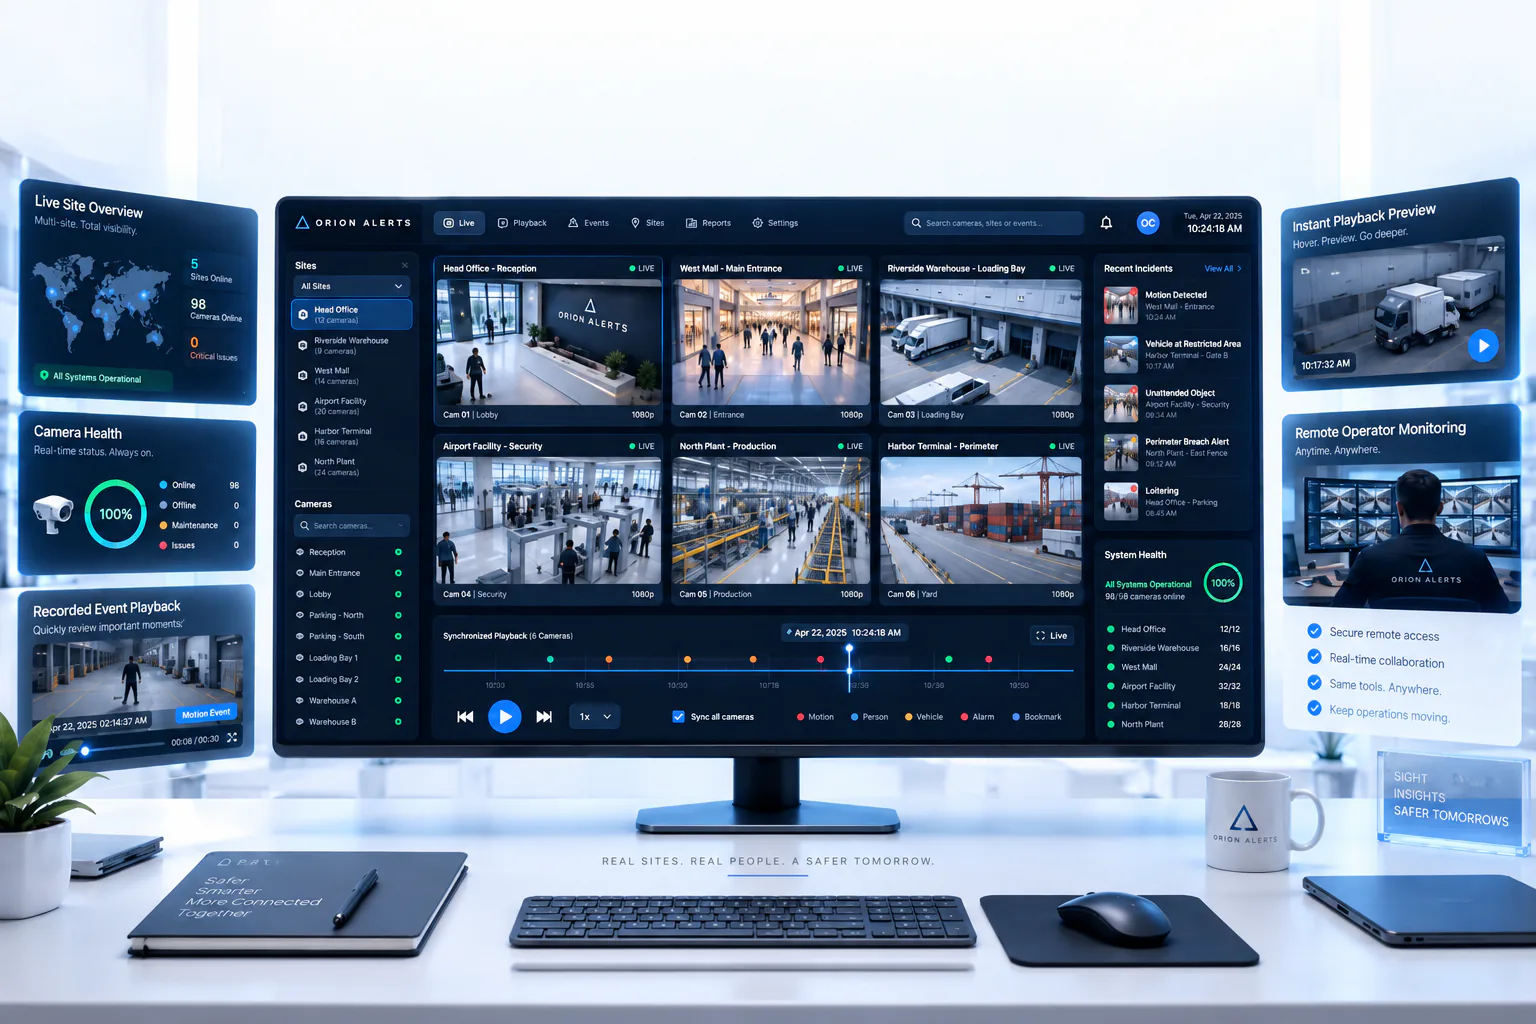
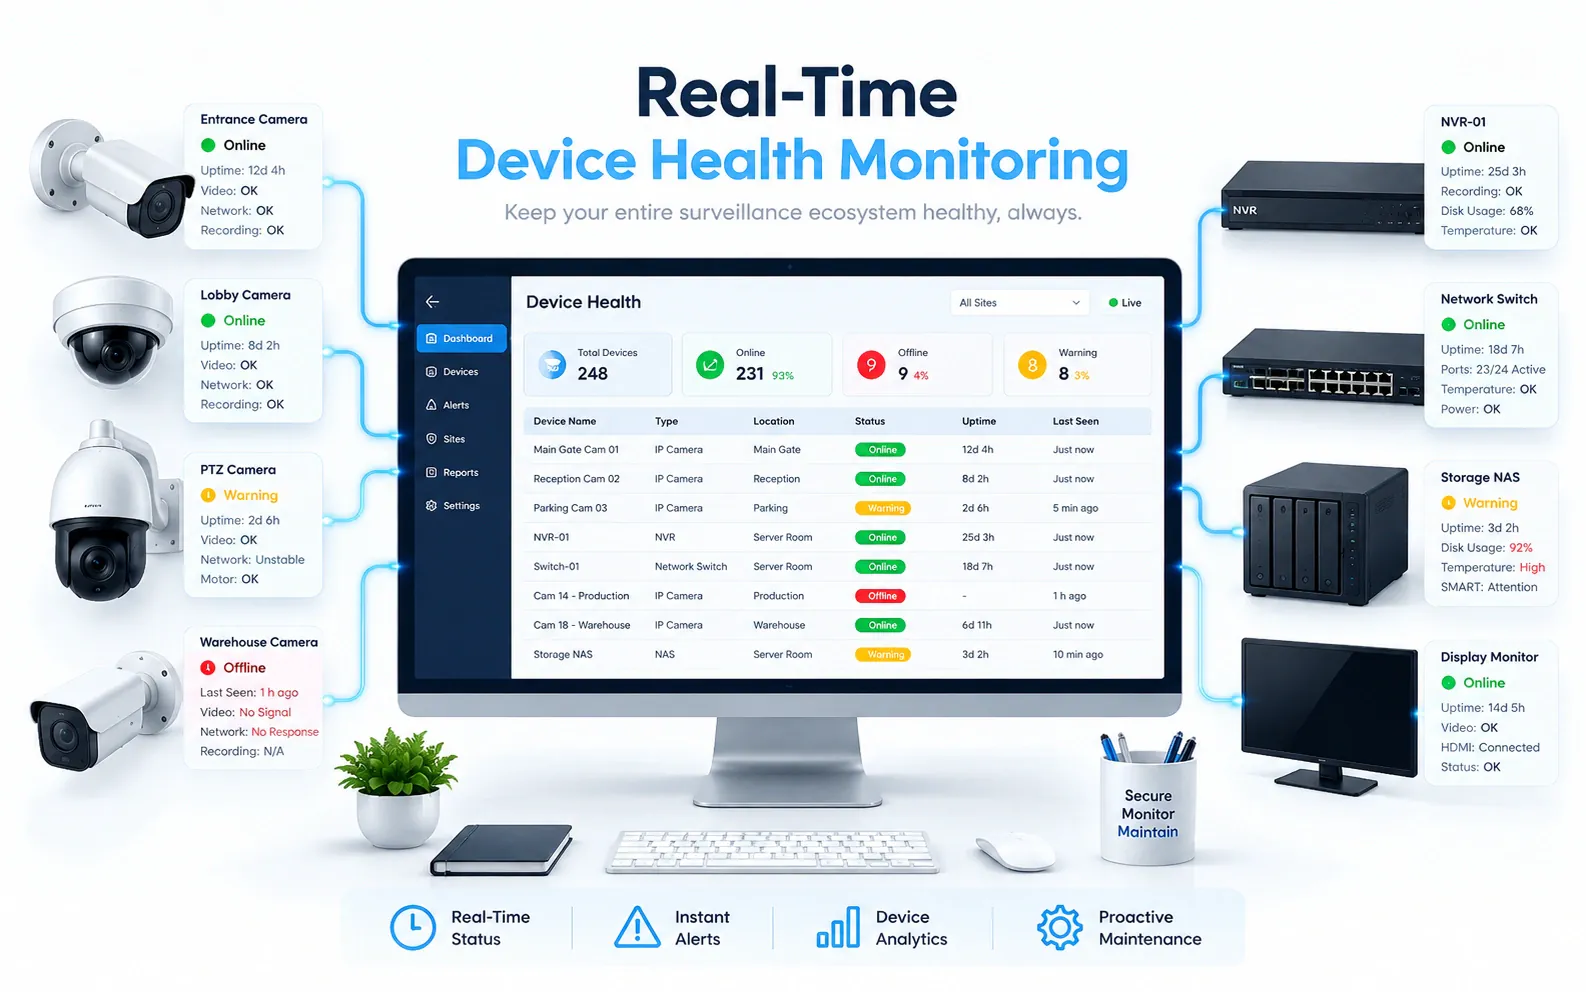
Manufacturing · Questions
AI video analytics for factories: common questions
What can AI video analytics detect on a factory floor?
Typical starting points are missing helmets or hi-vis vests at production entries, people entering configured machine or maintenance zones, and material piling up at a transfer point; pedestrians in vehicle lanes can be assessed in a pilot. Alerts reach the production supervisor or EHS with the clip and location. Machine OEE and product quality need production-system data.
Who receives factory alerts, and how?
Alerts go to the team that owns the area, typically the production supervisor and EHS for PPE and material-flow events. Each alert arrives on the dashboard, mobile app and email with the camera, location and clip, and the pilot agrees who handles camera outages before rollout.
How does Vision Copilot help at shift handover?
A supervisor can ask what the plant team should review before the next shift. Vision Copilot answers from observations in the mapped zones, for example material build-up recurring at one transfer point during handover, and suggests a next step such as checking staging space and replenishment timing.
Can AI video analytics calculate OEE from CCTV?
Not on its own: video shows visible stoppages and material build-up that add context to OEE losses. OEE itself needs defined availability, performance and quality data from your production systems, so linking camera observations to OEE is treated as a separate integration scope, agreed after the safety and flow pilot.
Does PPE detection prove compliance?
No. It flags selected visible PPE exceptions, such as a missing helmet or hi-vis vest, at defined entry points for a supervisor to review. It cannot confirm every item, correct fit or equipment condition, so those checks, and full legal compliance, stay with your site's own inspections and safety processes.
Where should a pilot begin?
Choose one well-lit entrance, a clearly defined restricted area and an accountable response team. Test the views across every shift, including low light and occlusion, and agree who receives each alert and how camera outages are handled. Expand only after representative shifts have been reviewed with the production supervisor and EHS.
Can we use our existing CCTV cameras?
Yes, in most cases: OrionAlerts connects to compatible IP cameras and recorders through ONVIF, RTSP and vendor SDKs, so working hardware can usually stay in place. A short assessment checks camera position, image quality and network access for each use case, and confirms compatibility model by model before the pilot starts.
Where is the video stored, and who can see it?
On site: video and AI inference stay on the on-site node, while Orion Cloud syncs alerts, health status and configuration metadata for central management. Role-based access means each user sees only the sites, cameras and functions in their scope, and retention is set per camera, zone or site to follow your own policy.
Manufacturing · Further reading
Further reading for factory teams
Manufacturing · Related
Industries related to factories
Ask Vision Copilot about your plant.
Start with one production entry, one crossing and one transfer point on cameras you already have.